machining · welding · cleanroom · test
One way, no backtracking
A single-direction process, audited at every zone.
Schedule a line walkSeven zones, one direction
Raw material in · packed parts out · no return path
1 · Raw material
Intake
Material is booked in against its heat number. That log is the thread every later record points back to.
2 · CNC
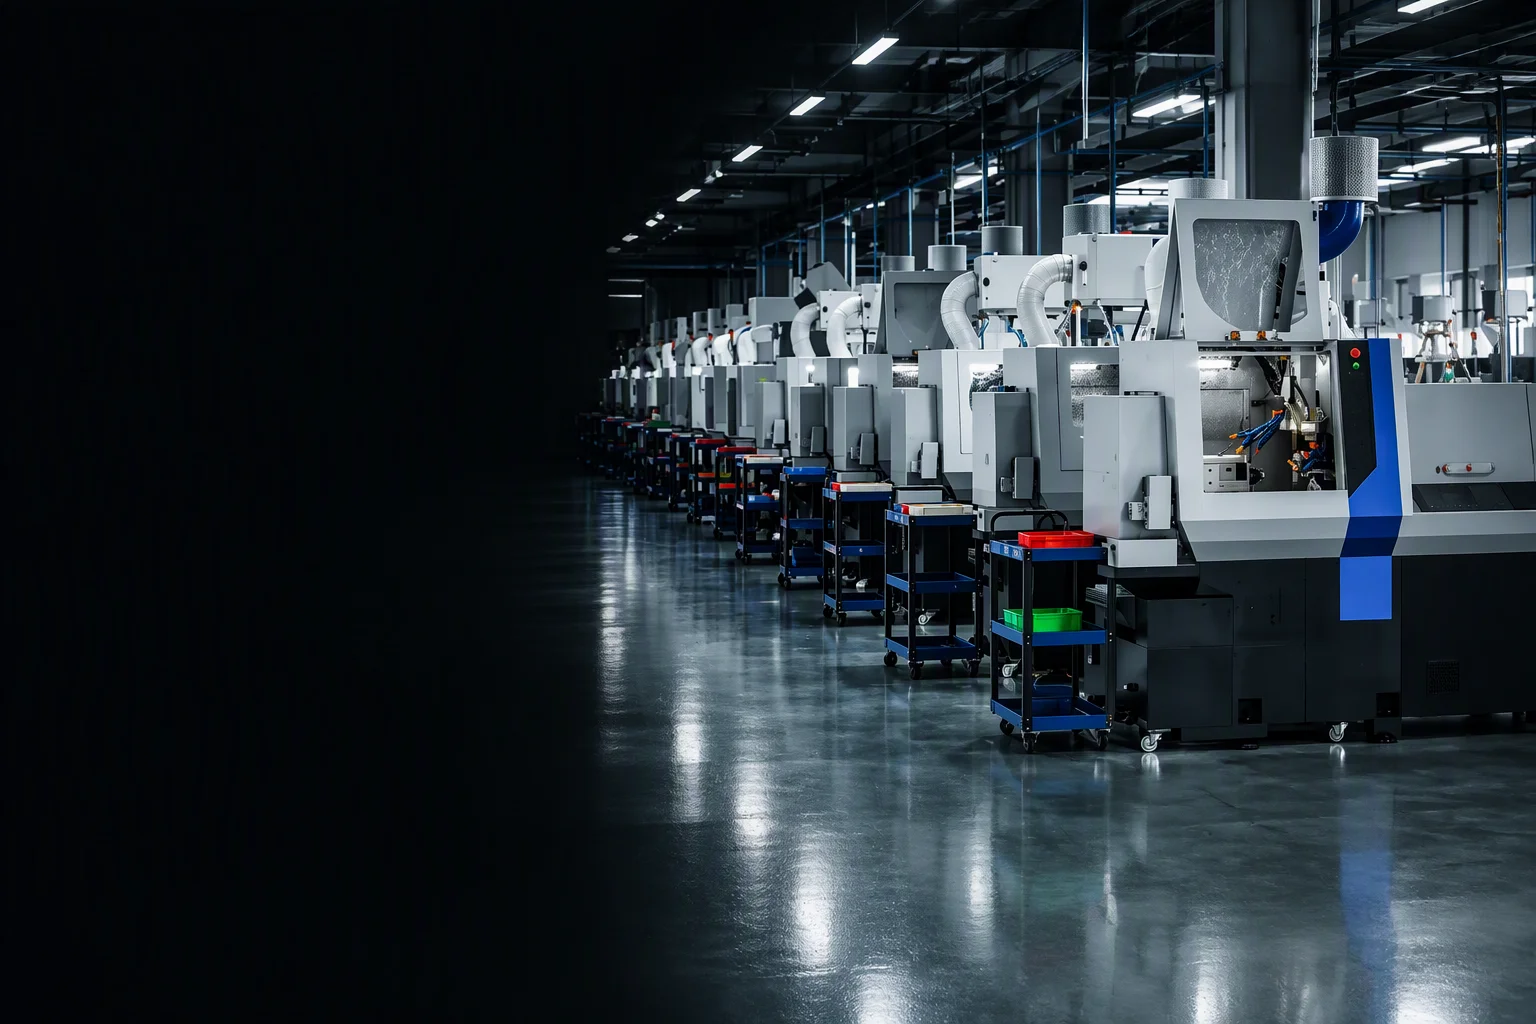
Precision machining
Bodies and seal seats are machined from 303 stainless and 304 stainless, the grades this class of part is machined in. industry practice
3 · Welding
Welding unit
Manifold headers and coupling bodies are joined in a dedicated unit, then routed to finishing. See the welding page.
4 · Finishing
Surface and passivation
Surface treatment and passivation before any part is allowed near the clean side.
5 · Cleanroom
Clean assembly
Semiconductor-grade clean assembly. industry practice The zone is described below, and in detail on the cleanroom assembly page.
6 · Test
In-house benches
Four bench types sit at the end of the line. What each one measures is below; the acceptance bands belong to the quality page.
7 · Packing
Clean packing
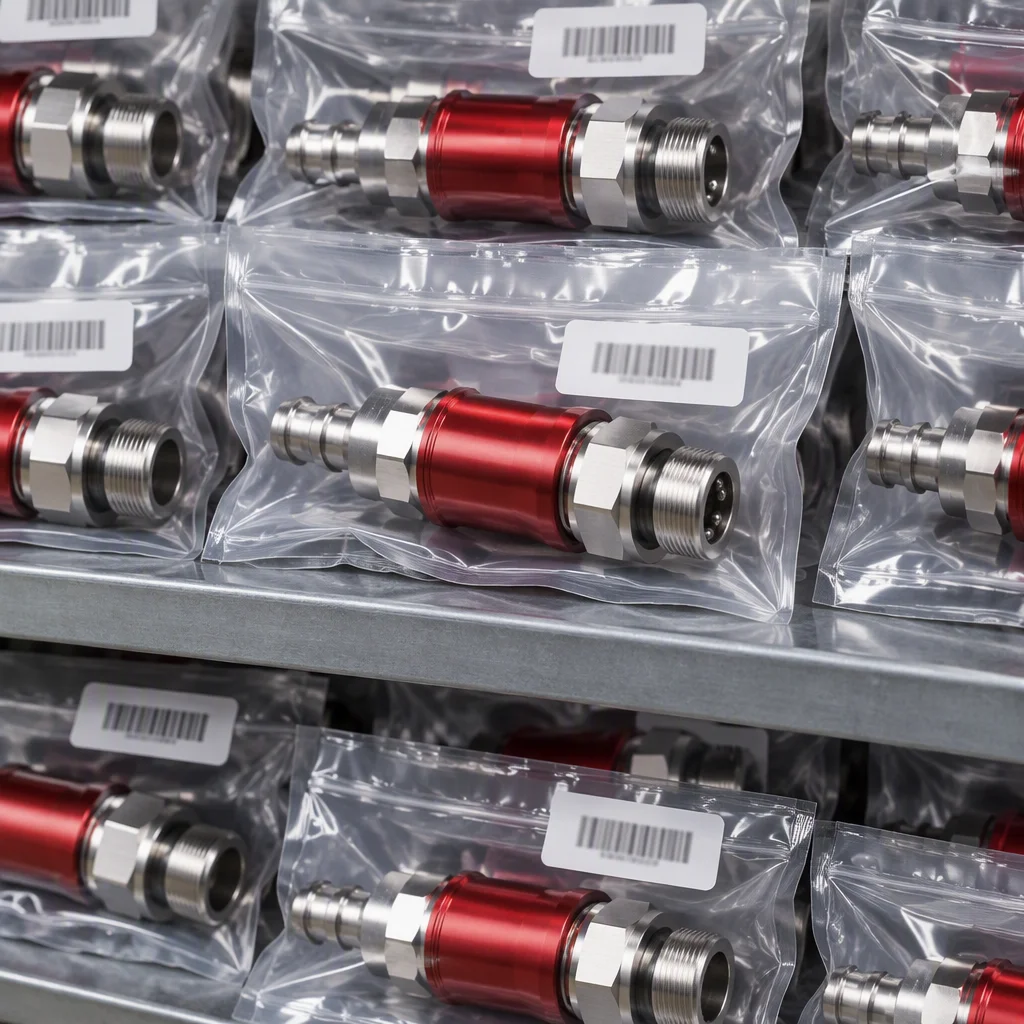
Dust plugs, clean-compatible packing and a laser-marked serial before anything leaves the building.
One-direction flow: material does not go back. Rework leaves the line at a separate lane and is recorded like any other movement. That lane is the marked branch on the drawing above.
Both lines, one record
2 lines · 1 record · shared traceability
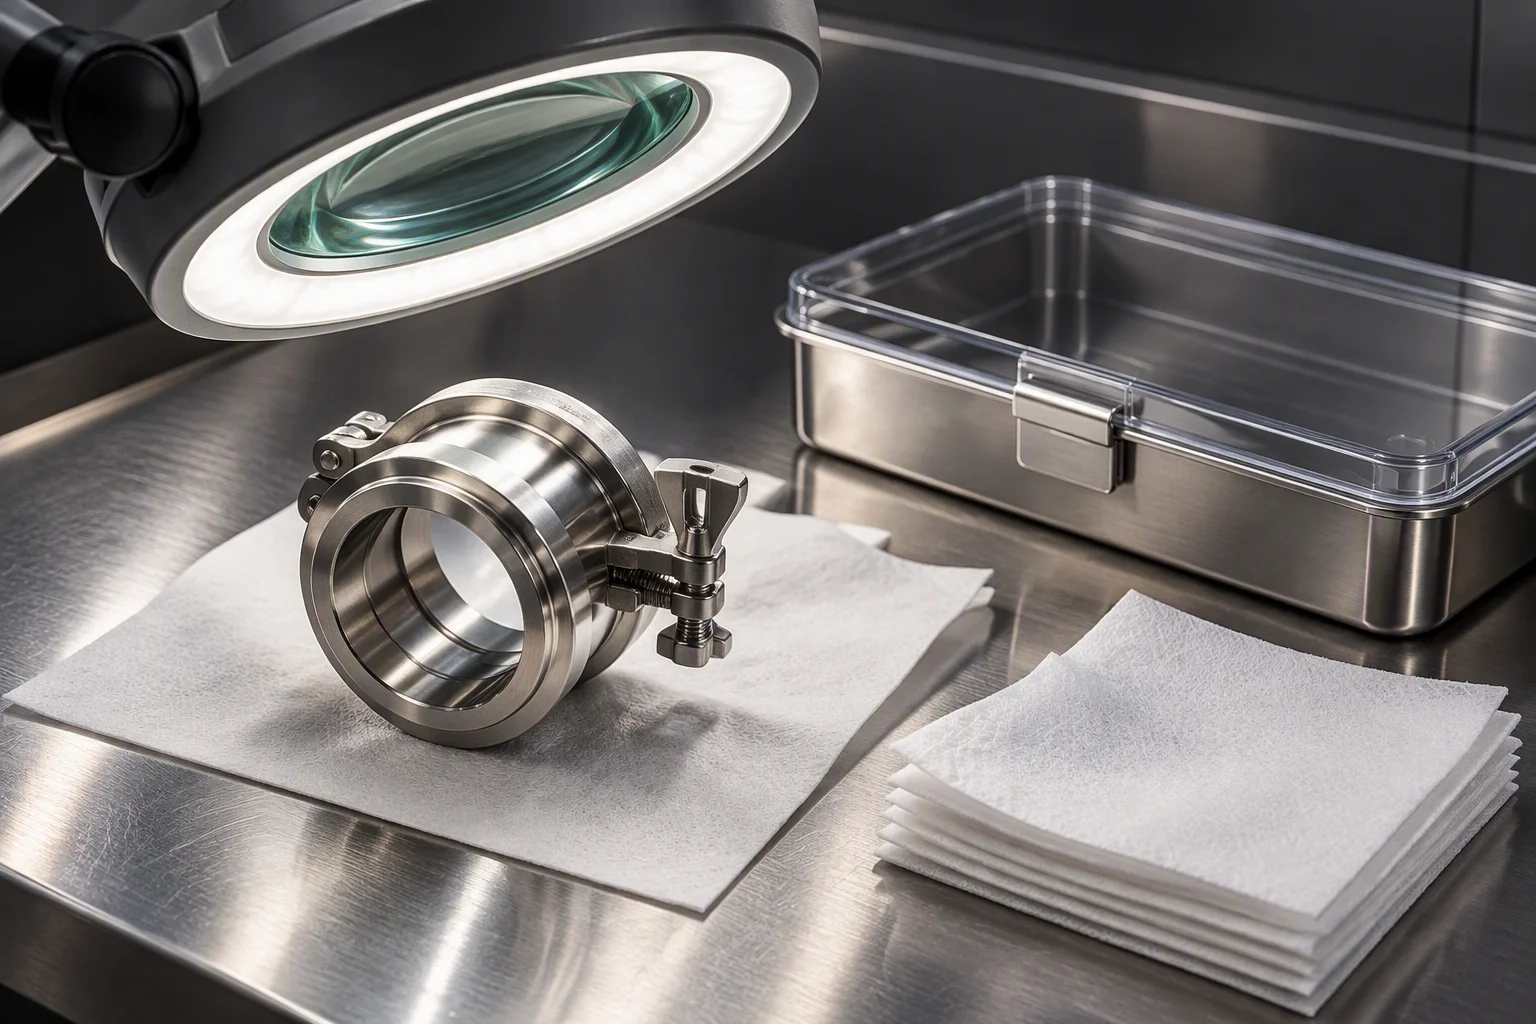
Cleanroom assembly, as practised
Industry practice · gowning · monitoring
Industry practice
Semiconductor-grade clean assembly and shipping verification, the practice this product class is held to rather than a class number borrowed from another industry. industry practice
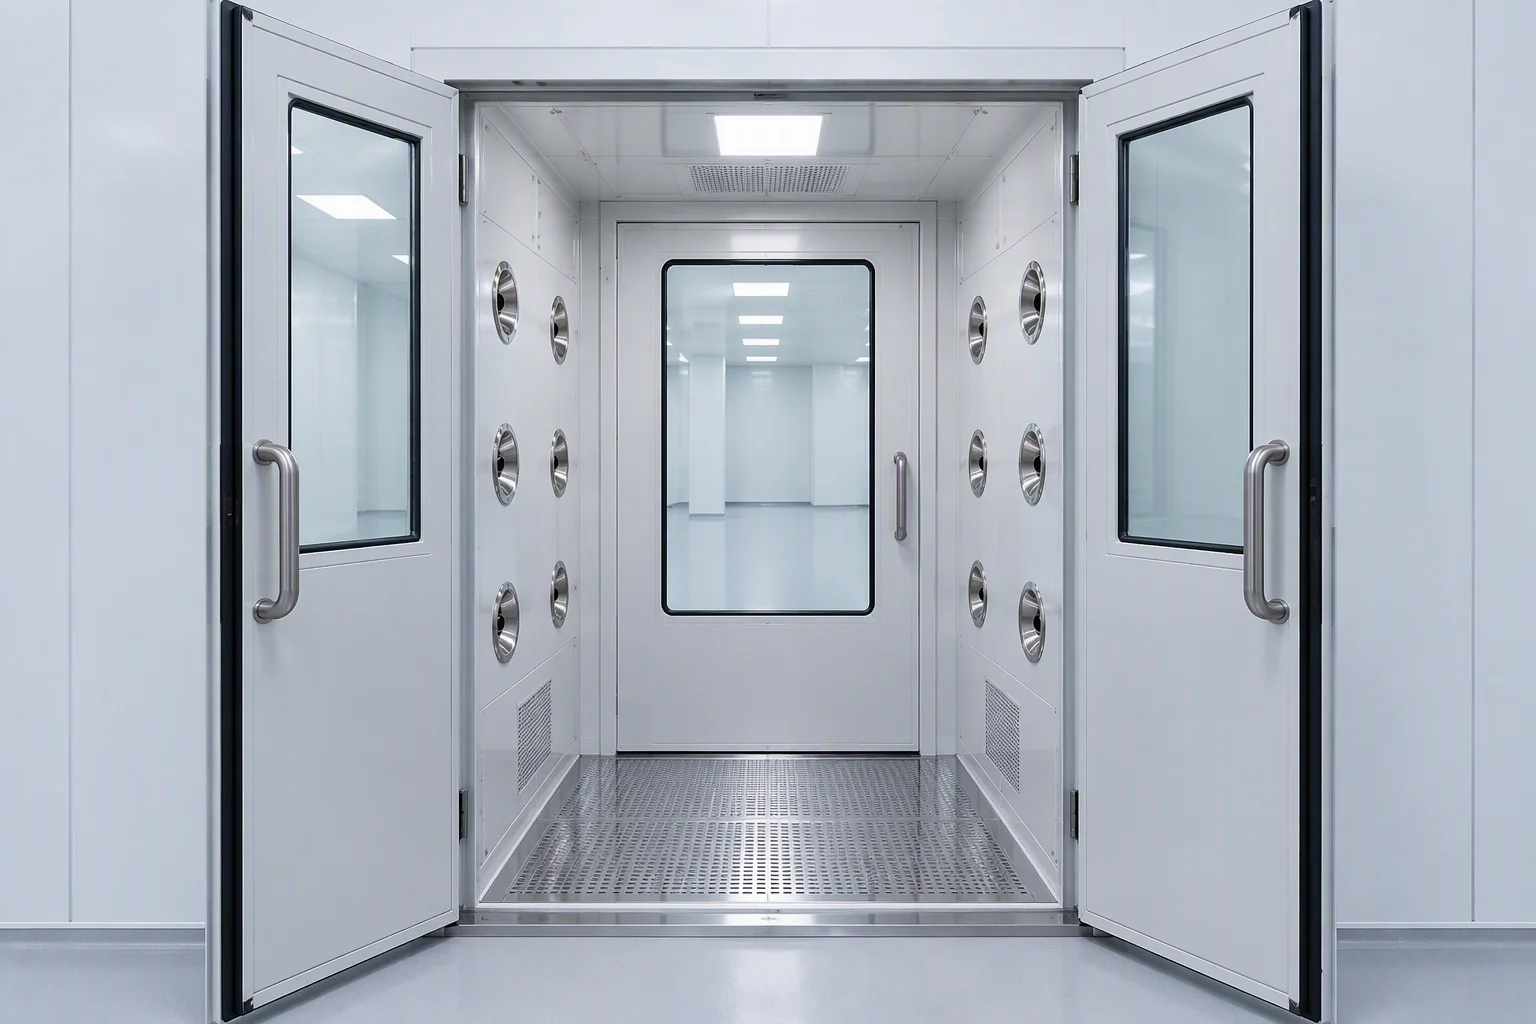
Gowning & transfer
Gowning and transfer protocols are followed at the entry, so the entry is a controlled step rather than a doorway that happens to be closed.
Monitoring
Environmental monitoring is recorded against procedure. No cleanroom class figure is claimed on this page.
What the in-house lab runs
Four bench types · per-part discipline
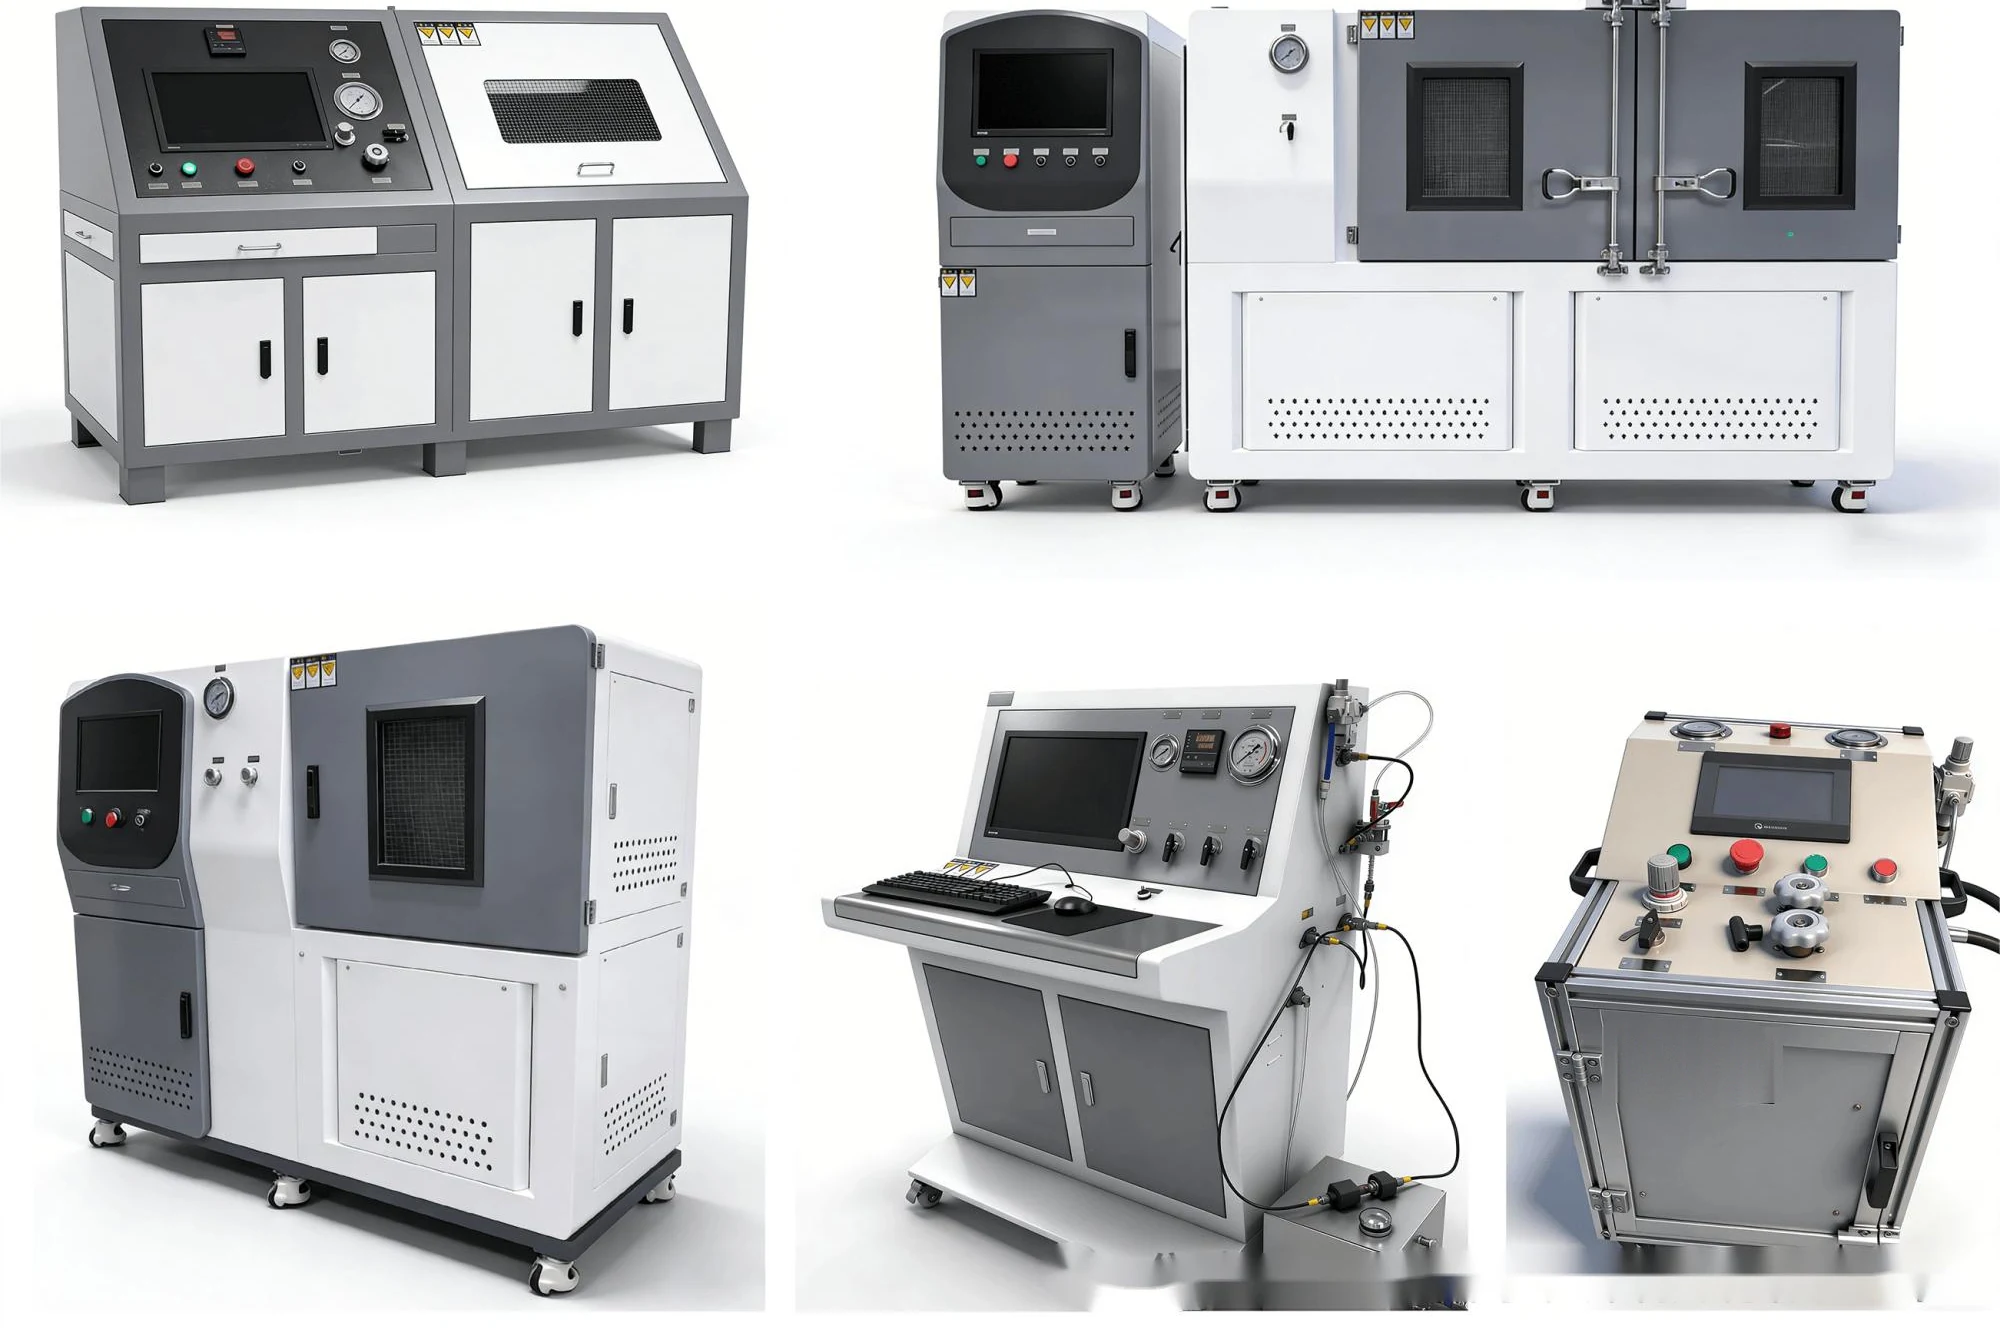
The bench set: control console, environmental chamber, pressure cabinet and two instrumented benches, shown as an equipment set rather than as a photograph of a room. Per-part leak testing is the practice this class of supplier is held to. industry practice The benches are duplicated at the end of the line, and each one carries its calibration schedule on the bench itself.
What the line tests is here; how the results are judged, and to which standard, is on the quality page.
System reference and traceability
Capability wording · document control · serials
System reference
Connector manufacturers of this class run ISO 9001 and ISO 13485 systems. industry benchmark This page states the alignment rather than the paperwork: an ISO 9001-aligned process, with no document numbers, no scans and no legal entity named on this site.
Document control
Document control and corrective action are in place, and internal audits run on a fixed calendar rather than when a customer asks.
Traceability
Laser-marked serials, with lots traceable back to the heat number the material was booked in under. The record travels with the batch.
Packing
Dust plugs and clean-compatible packing before dispatch, so the last zone does not undo the fifth.
Equipment the zones are built from
Machining and process cells · finishing and forming
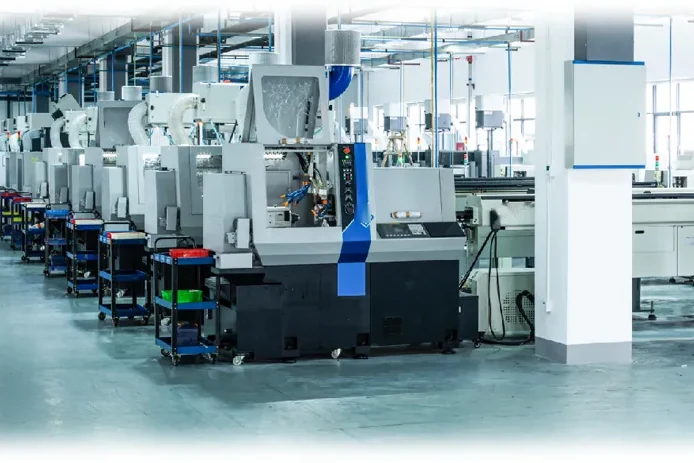
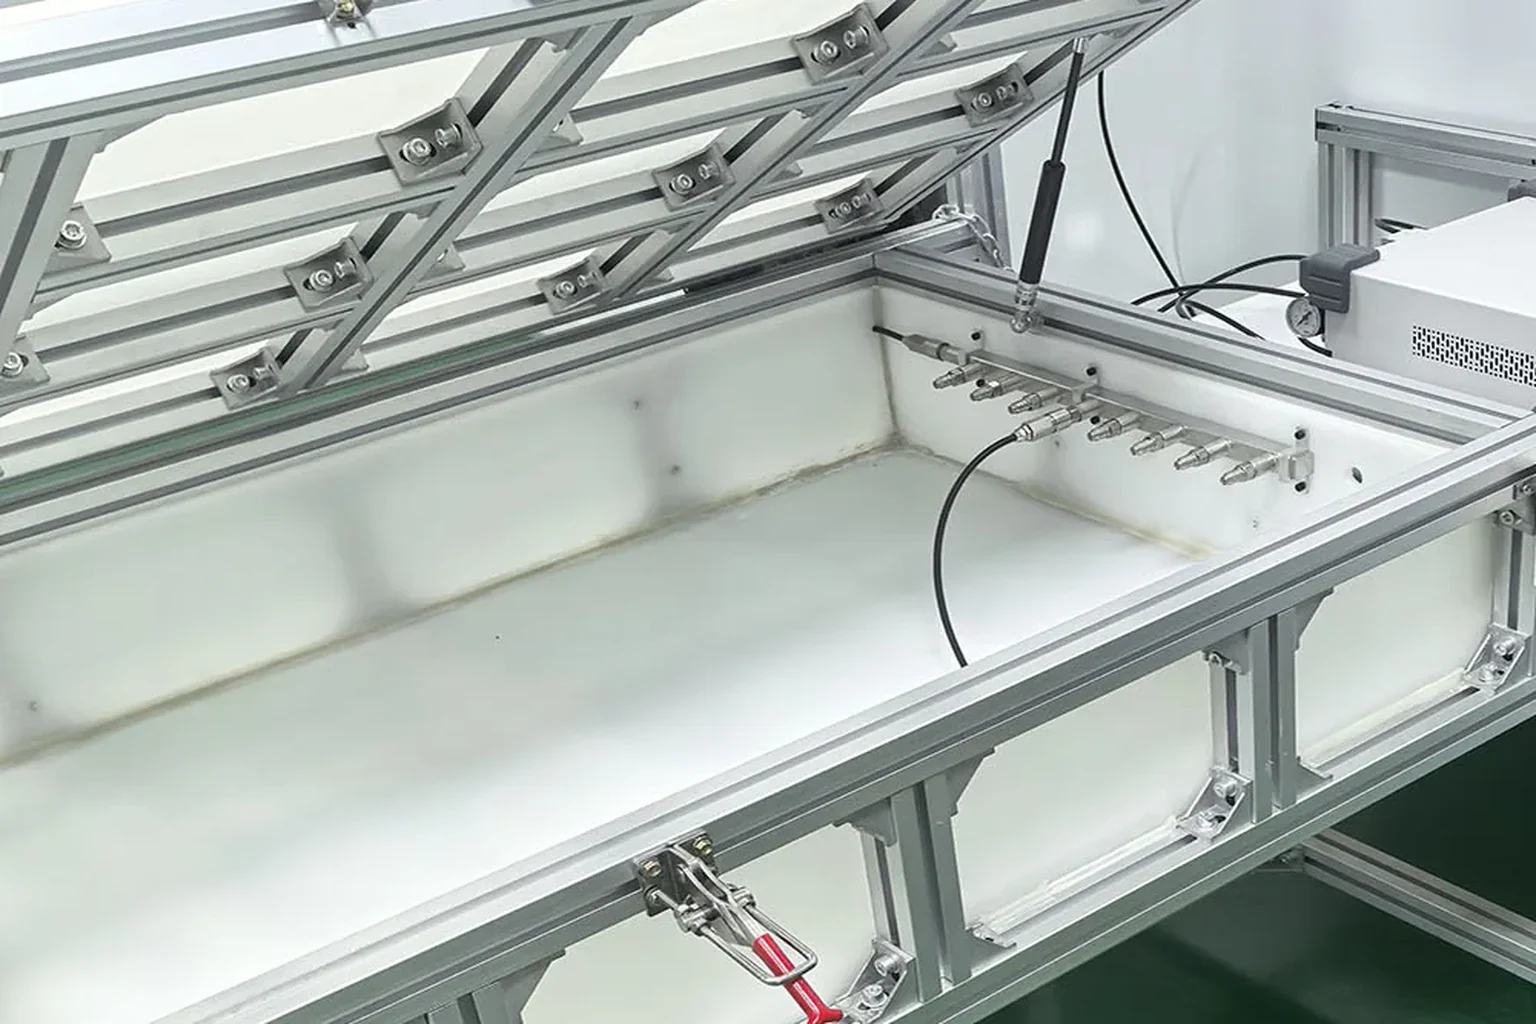
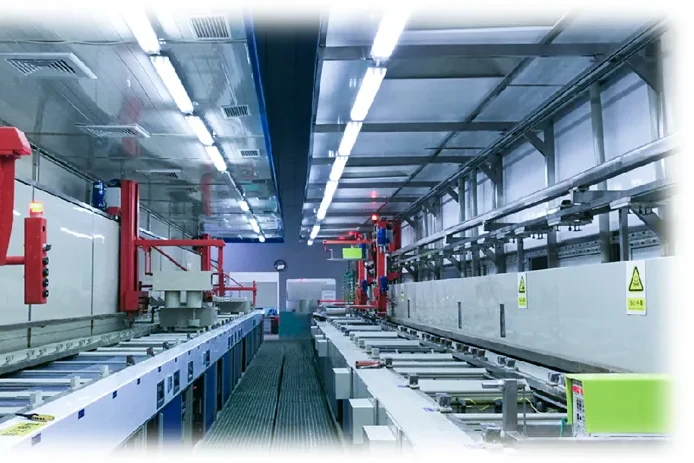
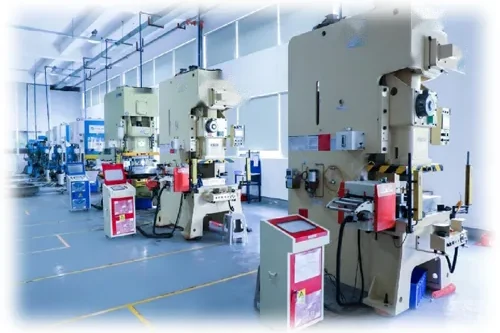
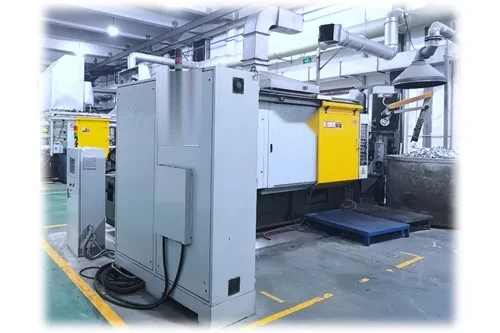
The forming and casting cells feed the machining zones rather than sitting inside the seven-zone path. The machining route itself, down to the seal-face finish, is on the precision CNC page; the wider set of processes is on capabilities.
Line walk
Walk the line, from your desk.
Ask for a live walk-through or a recorded audit of the zone you care about, against an ISO 9001-aligned process and the records behind each batch. Staged delivery and first-article work are handled on the project support page.
Schedule a line walk One business day · English quote + a one-page spec sheet